Paper Packaging Factory Innovations That Reduce Waste and Lower Costs
2026-11-16
Every year, paper packaging factories face the same tension: how to trim material waste without inflating production costs. At Imagine Craft Packaging, we've watched this challenge reshape shop floors and supply chains alike. The innovations that actually stick aren't flashy one-offs—they're quiet changes in cutting patterns, adhesive formulas, and machine timing that compound into real savings. In this post, we'll walk through the practical upgrades and mindset shifts that help factories ship lighter, spend less, and leave fewer scraps behind.
Cutting Maps That Squeeze More Cartons From Every Sheet
Every corrugated sheet hides untapped potential, and the right cutting map turns that potential into profit. Instead of accepting standard layouts, we analyze flute direction, scoring allowances, and blank orientation to nest cartons with almost zero waste. Small shifts in rotation or mixed-size pairing often recover enough board to add an extra carton per sheet, which compounds across a full production run.
The difference shows up where it matters most: the trim bin. By harmonizing knife paths and reducing scrap strips between blanks, operators see fewer skeleton leftovers and faster setup changes. A well-designed map also accounts for die-cut features like hand holes and lock tabs, so structural integrity is never sacrificed for material savings.
Real gains come from treating the cutting map as a living document. As order mixes shift, reworking the layout with fresh nesting logic can reveal hidden capacity. Teams that revisit maps quarterly, not yearly, routinely uncover 3–7% more cartons from the same sheet stock without touching machine speed or board grade.
Closed-Loop Rinse Water Cuts Treatment and Supply Costs
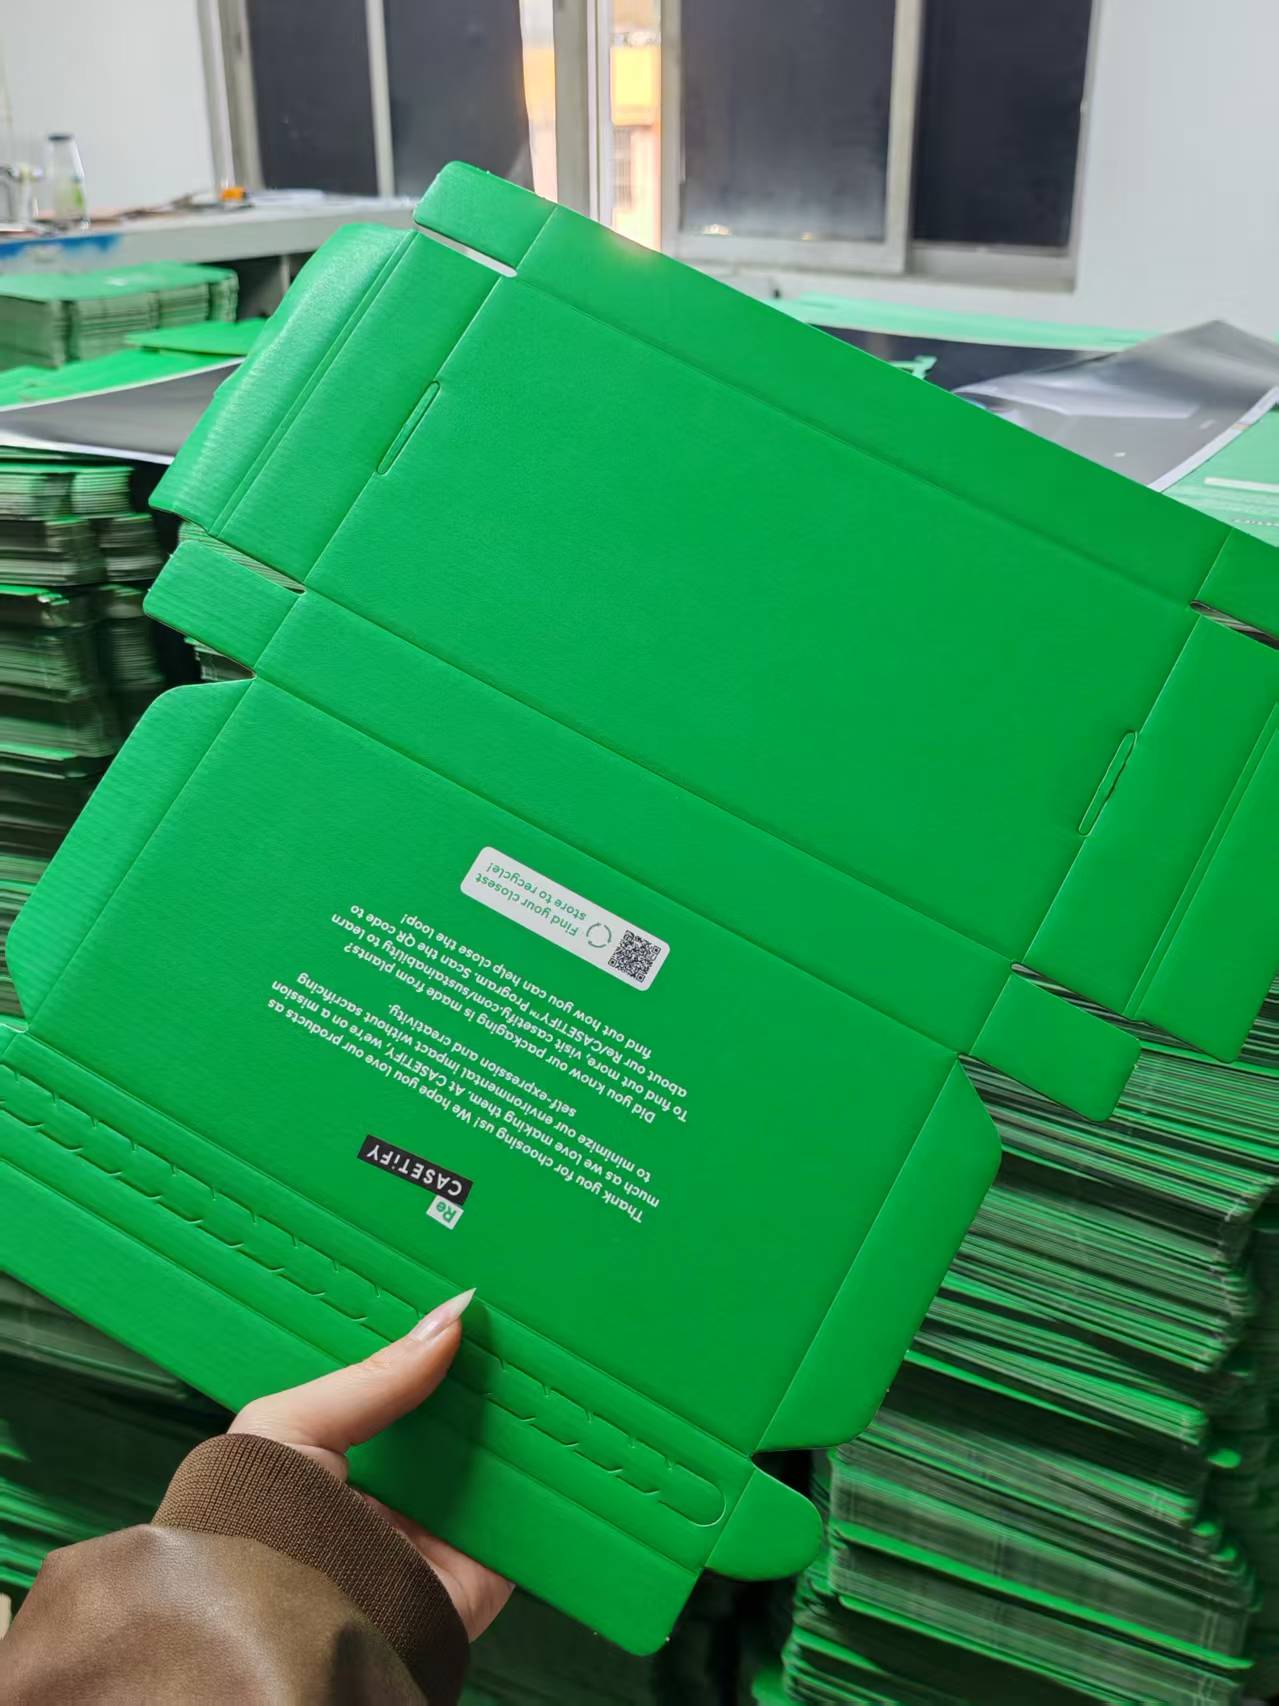
Rinsing steps in metal finishing, electronics assembly, or food processing often pull fresh water from the municipal line, then send the lightly contaminated discharge straight to treatment. A closed-loop rinse system changes that logic: after each rinse cycle, the water passes through filtration or membrane separation, gets topped up to replace drag-out losses, and returns to the line. The immediate result is that a facility can cut its rinse water intake by 70 to 95 percent depending on the process chemistry and layout.
Treatment costs drop for a less obvious reason. Since the same water recirculates, contaminants concentrate in a controlled loop rather than flooding the wastewater stream with large volumes of dilute effluent. That means smaller holding tanks, less coagulant or pH adjustment chemical, and fewer surcharges from the local utility. Supply costs also shrink because the plant no longer has to soften or heat an endless stream of incoming water; it only conditions the relatively small replacement volume. Over a year, plants often recover the cost of the recycling skid through lower water, sewer, and energy bills.
Waste Dryer Heat Now Preheats Incoming Air and Water
Capturing the heat that would otherwise leave through the dryer exhaust is one of the easiest wins in a laundry operation. Instead of letting that energy escape, a well-designed recovery loop routes it back to where it matters most: the incoming air stream and the cold water supply. This means the dryer doesn't have to work as hard to reach its target temperature, and the wash cycle starts with warmer water before any additional heating kicks in.
The setup typically involves a heat exchanger that sits directly in the exhaust path. As hot, moisture-laden air passes over one side of the exchanger, fresh incoming air or incoming water flows over the other side, absorbing that thermal energy without ever mixing with the exhaust. It's a straightforward pass-through design that requires no moving parts beyond the existing blowers, and it can be retrofitted into most existing dryer banks with minimal downtime.
Operators often notice the difference within the first billing cycle. Dryer cycles shorten slightly because the preheated air reaches evaporation temperature faster, and water heating costs drop by a measurable margin since the incoming water is already lukewarm before the boiler sees it. Over a year, that recovered heat quietly shaves thousands off the utility bill without any change in how the staff loads or runs the machines.
Digital Print Runs Remove Plate Setup Scrap Entirely
In conventional offset work, every job starts with plate making—bending, mounting, and then pulling sheets until registration and color settle. None of that exists in a digital run. The file goes straight to the imaging unit, so the first sheet out can be a saleable sheet. There is no stack of waste that gets counted against the job.
Because there is no plate to burn or clean, short runs stop carrying a hidden setup penalty. You can print fifty copies of a revised brochure, then switch to a completely different piece without stopping to strip and re-mount anything. That speed changes how people think about inventory and reprints.
The scrap savings go beyond paper. No plate chemistry, no fountain solution carryover, no plate storage at the end. A digital press may still need calibration, but it does not generate the same kind of predictable startup waste that a plate-based press does on every job change.
Thinner Yet Stronger Board Uses Less Fiber per Box
Most corrugated board gets its rigidity from the thickness of the fluting, but that approach wastes fiber. By shifting to a denser, micro-crushed flute profile, the board loses nearly a quarter of its caliper while actually gaining edge crush strength. It's a counterintuitive move: less material in the middle, yet the box holds up better under stacking pressure.
The practical payoff shows up quickly on the production floor. Each container now pulls fewer square meters of liner and medium from the roll, which means a single ton of virgin or recycled fiber stretches into more finished boxes. Freight costs dip because the same truck can carry more knockdowns, and warehouse racks feel the difference too. This isn't just lightweighting for its own sake — it's a direct cut in raw material demand per unit, without asking customers to accept a flimsier carton.
Vibration Sensors Catch Bearing Wear Before It Halts a Line
On a busy packaging line, a bearing can degrade for weeks before anyone notices. The first sign might be a faint high-frequency vibration that only a trained ear—or a well-placed sensor—can pick up. By the time heat builds or noise becomes obvious, the damage is already done: scored races, spalled balls, and an unplanned shutdown that ripples through production. Vibration sensors change that narrative. They listen continuously, capturing the early signatures of wear that precede catastrophic failure, and send alerts when the pattern deviates from a healthy baseline.
The key is in the frequency spectrum. A healthy bearing produces a predictable vibration signature. As wear progresses, tiny defects on the raceway or rolling elements generate repeating impacts at specific fault frequencies. Piezoelectric accelerometers mounted on the bearing housing convert those mechanical pulses into electrical signals. Onboard processing or edge gateways then run fast Fourier transforms to isolate the telltale peaks. A shift in the high-frequency band—often above 2 kHz—can indicate lubrication breakdown or early spalling, long before the bearing seizes. Maintenance teams get a clear, data-driven heads-up instead of relying on walk-around inspections with a handheld meter.
What makes this approach stand out is not just detection but decision support. Instead of replacing every bearing on a fixed schedule, plants can monitor actual condition and schedule intervention only when needed. Some systems even track the progression rate of the fault frequency, estimating remaining useful life. That turns a reactive scramble into a planned, two-hour swap during a shift change. The line keeps running, and the bearing never gets the chance to halt it.
FAQ
Lightweight corrugated board designs now use less fiber while preserving crush resistance, and computer-based nesting software squeezes more blanks onto each sheet. Many plants also mount sensors on glue applicators to trim adhesive use by up to 18%, which keeps both waste and raw material spend down.
A practical route is to install variable frequency drives on motors and capture heat from drying tunnels for preheating wash water. One mill I know cut its gas bill by around 14% just by reclaiming exhaust heat from the corrugator and using it to warm the facility during winter months.
Switching from solvent-based to water-based inks is a good example. It removes hazardous waste disposal fees, reduces ventilation energy, and lets operators clean plates with mild soap instead of expensive solvents. Most plants can make that change without buying new presses.
In-line vision systems now check print registration, glue patterns, and board dimensions at full line speed. When something drifts outside tolerance, the system flags the stack immediately, so you reject a few sheets instead of discovering a problem after an entire pallet has been wrapped and shipped.
They take rinse water from printing and maintenance areas, filter out ink solids and fibers, and return clean water for reuse. That can cut a plant's water intake by 40% or more, lower sewage fees, and shrink the volume of sludge that has to be hauled away.
Right-sized packaging is the quiet winner here. Instead of shipping air, designers use data from order histories to create boxes that fit the product more closely. That reduces corrugated use per unit, cuts shipping weight for the customer, and lowers the factory's board consumption without sacrificing protection.
Yes, because unplanned stops often leave half-processed board sitting on the line, which usually ends up as scrap. By monitoring vibration, temperature, and oil condition on critical motors and rollers, maintenance teams can replace parts during planned windows and avoid those sudden jams that ruin batches and force overtime.
Conclusion
Paper packaging factories are rethinking everyday processes to trim both material waste and operating expenses. Instead of accepting standard sheet layouts, cutting maps are now optimized to squeeze more cartons from every sheet, which directly reduces the amount of board purchased. At the same time, rinse water from cleaning operations is being captured, filtered, and reused in a closed loop, so facilities pay less for incoming water and also cut the volume of wastewater that needs treatment. Heat that used to escape from dryers is no longer wasted either; it's routed to preheat incoming air and water, lowering the energy needed to bring them up to temperature. These changes may sound modest individually, but together they take a noticeable bite out of monthly utility and material bills.
On the production floor, digital printing is eliminating plate setup scrap entirely, since jobs go straight from file to substrate without making plates or running test sheets. Material science is helping too: a thinner yet stronger board uses less fiber per box while still protecting products during shipping. And to keep lines running smoothly, vibration sensors monitor bearings continuously, catching early wear before it turns into an unexpected breakdown that halts production and generates waste. These upgrades don't just reduce waste; they make the whole operation more predictable and less dependent on emergency fixes. The result is a leaner factory where cost savings come from smarter daily decisions rather than large capital projects.
Contact Us
Contact Person: Sunnie
Email: [email protected]
Tel/WhatsApp: +8615818596517
Website: https://www.imagine-craft.com/