Roto Moulding Machine Solutions That Deliver Consistent Product Quality
2026-11-19
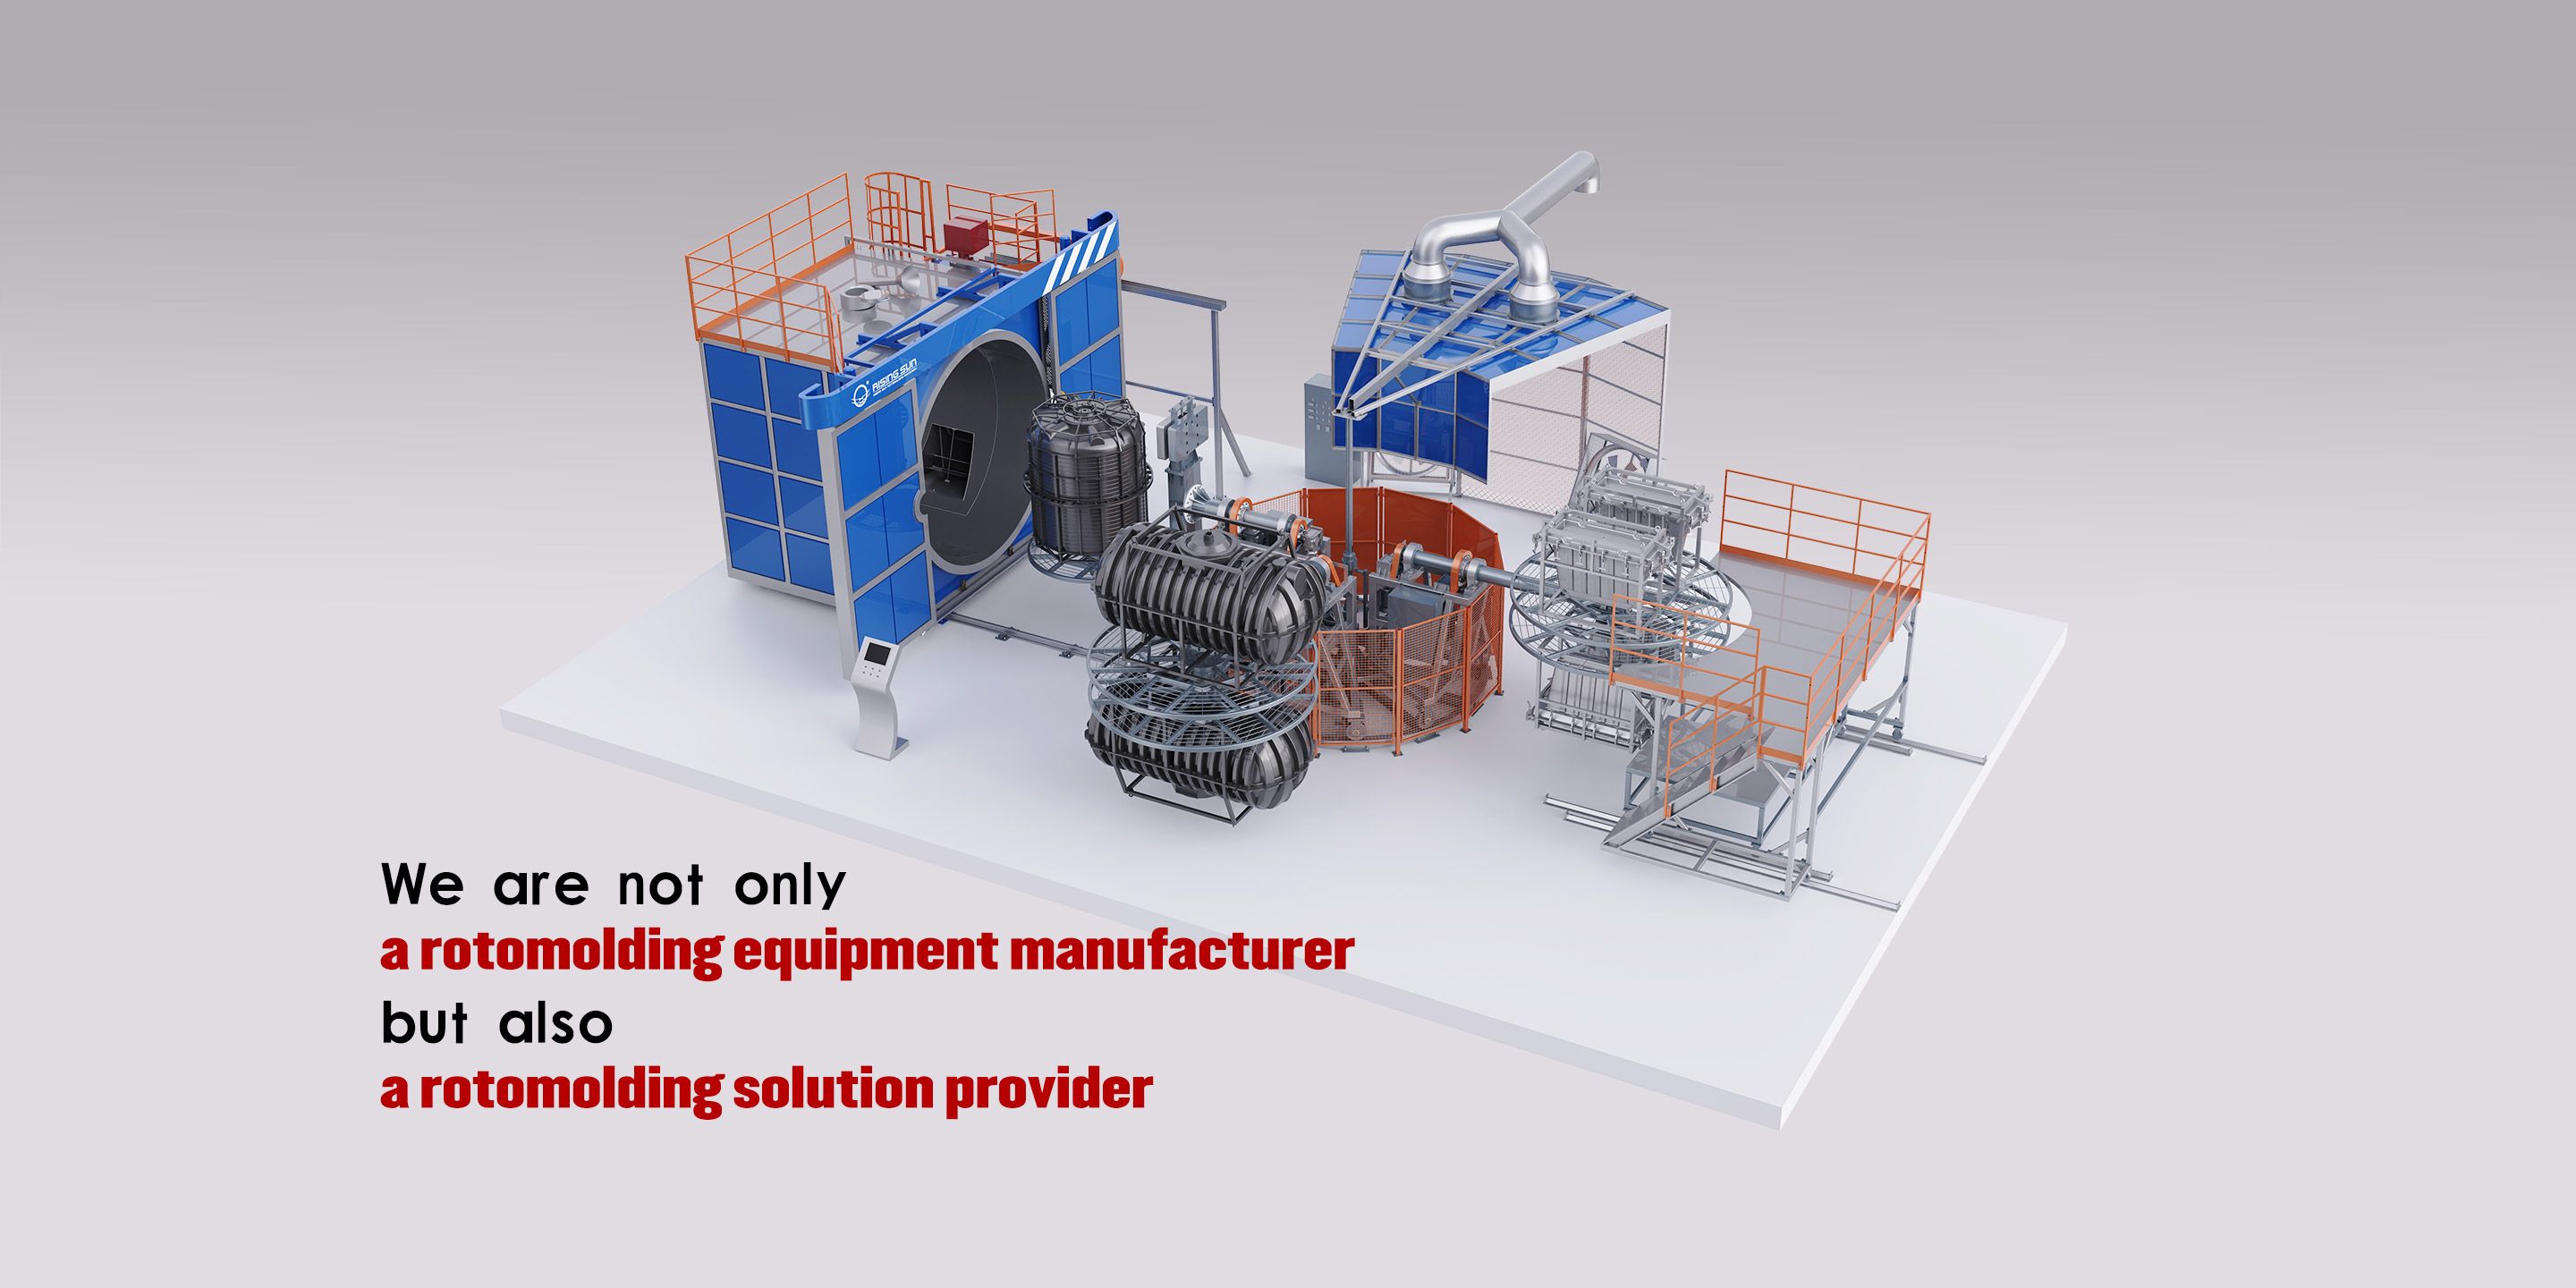
When a rotomoulding line runs slightly off-spec, the cost rarely shows up on the first inspection. It hides in inconsistent wall thickness, warped lids, or a tank that fails after two seasons in the sun. That is why the conversation has shifted from ‘What machine can we buy?’ to ‘Which rotomoulding partner can make quality repeatable at every cycle?’ At Rising Sun, we build answers around that harder question—with machine designs and process control aimed not just at output, but at the kind of part consistency that protects your reputation. This blog looks at the practical ways the right rotomoulding machine changes what you can promise your own customers.
Why Uniform Wall Thickness Depends on More Than Machine Settings
Machine settings like barrel temperature, injection speed, and hold pressure are often treated as the primary controls for wall thickness consistency, but they operate on a melt that has already been shaped by decisions made upstream. The polymer enters a cavity through gates and runners whose size, position, and balance dictate how the flow front advances and where it stalls. If the flow path forces material to travel much farther in one region than another, no amount of screw adjustment can fully erase the resulting pressure drop and premature solidification.
Part geometry plays a quieter but decisive role. Ribs, bosses, holes, and abrupt transitions create local flow hesitations and differential cooling rates, pulling material away from the nominal wall before packing can compensate. A nominal 3 mm wall is only meaningful when the surrounding features allow the melt to reach every section at nearly the same time and temperature. Designers often discover that thinning a thick boss or relocating a gate does more for consistency than tightening process windows.
Cooling and shrinkage finish the story. Even with a balanced fill, uneven heat removal from the core and cavity sides can bow or sink a part, changing the effective wall after ejection. Tool steel selection, cooling line placement, and ejection timing become part of the thickness equation because the part continues to move and contract long after the screw stops. Uniform walls are therefore an outcome of geometry, tooling, and processing decisions working together, not a dial that can be set on a controller.
Keeping Heat and Cooling Cycles From Drifting Over a Run
The body's thermostat rarely stays put during longer efforts. Early miles often feel cold because blood flow is still weighted toward working muscles, then a sharp rise in core temperature arrives once the pace settles. That lag invites a familiar overcorrection: stripping layers too soon, sweating heavily, and then getting chilled when the effort drops or the wind picks up. Keeping the cycle from drifting starts with accepting that thermal comfort is a moving target, not a setting you lock in once.
Small, repeatable adjustments matter more than big gear changes. Unzip a vent before you feel hot, tuck a glove away before your hands go numb, and ease off for a minute when your skin goes clammy. These tiny corrections prevent the swing between overheating and shivering that drains energy late in a run. A cap or headband that can be pocketed, a top that breathes without flapping, and a midlayer that holds just enough warmth when wet all help flatten the curve.
Pacing also plays a role. Surges push heat production above what sweat can handle, while a slow shuffle on a windy ridge can drop skin temperature quickly. Runners who drift less tend to treat effort, clothing, and exposure as one system: they adjust one variable before the others force a reaction. The goal is not to stay perfectly comfortable but to keep the swings small enough that the body spends energy on movement rather than fighting its own thermostat.
The Mould Design Details That Shape Part Quality
Gate placement and flow path geometry quietly set the ceiling for what a part can become. A gate shifted a few millimetres changes where polymer fronts meet, which determines weld line strength, sink mark visibility and the way fibres align under load. Rather than treating filling as a simple volume-to-volume event, it helps to think of every gate as deciding which regions cool under pressure and which regions lose packing before the material has frozen. In thin-walled work, that balance between hesitation and overpacking is often the difference between a dimensionally stable part and one that drifts after ejection.
Cooling circuit layout matters less for speed alone and more for how evenly heat leaves the cavity. When one side of a core runs hotter than the other, the part develops residual stress that may not show up until the component sits in service or passes through a secondary process like painting or bonding. Baffles, bubblers and the spacing of channels around deep ribs all shape local shrinkage rates. The goal is not always the fastest cycle time; it is a controlled, repeatable temperature field that allows the material to relax predictably before the mould opens.
Details at the parting line, vents and ejection points tend to leave fingerprints on the finished surface. Inadequate venting can burn the resin or force gas to the end of fill, while aggressive ejector placement can create stress whitening on textured surfaces or leave drag marks that catch light differently across a fascia. Small choices like adding a radius where a rib meets a wall, or moving a witness line to a low-visibility edge, often improve perceived quality without changing the part design. These are the details that separate a tool that merely fills from one that produces the same part consistently across thousands of shots.
Powder Handling Habits That Cut Down on Defects
Most powder-related defects don't start at the press. They begin the moment a drum is opened and the material meets air, moisture, and a rushed operator. One habit that consistently reduces scrap is conditioning the powder before it ever reaches the feed hopper. Letting material acclimate to the room for a few hours, sieving it through a mesh that matches the job, and avoiding aggressive shaking of containers keeps particle size distribution intact and prevents the fine segregation that later shows up as surface voids or weak knit lines.
Another overlooked practice is controlling how powder is returned to the system. Operators often scoop spillage back into the hopper without checking for contamination or humidity pickup. A simple change—using a dedicated, clearly labeled scoop for each material and keeping a lid on any staging container—cuts cross-contamination and moisture-related porosity. Equally important is monitoring the fill level in the feed hopper. Running it too low invites inconsistent flow and air entrapment, while overfilling can cause bridging. A steady, mid-range level helps maintain uniform density from shot to shot.
Housekeeping around the press also plays a bigger role than most teams admit. Dust that settles on tooling and tie bars can get knocked into the powder stream during mold changes or vibration. Wiping down surfaces with a damp, lint-free cloth before each setup and using vacuum systems instead of compressed air for cleanup prevents redistributing fine particles. These small, repeatable habits cost almost nothing but consistently lower defect rates in molding operations where powder handling is otherwise taken for granted.
Small Operator Routines That Prevent Process Shifts
Drift rarely announces itself. On a busy shift, a fixture bolt loosens a quarter turn, a cutting edge dulls just enough to push a bore toward the high side of tolerance, and a coolant concentration dips because nobody tops it off until morning. The routines that actually hold a process steady tend to be the small, almost unremarkable ones: wiping a locating surface before every load, checking a torque wrench against a marked line, or pausing to listen for a change in spindle pitch. Operators who do these things are not following a poster on the wall—they have turned the early warnings into physical habits.
One of the more effective patterns is a fixed checkpoint tied to part count rather than the clock. Instead of measuring when time allows, an operator might pull a dimension check on every tenth workpiece and record the result on a simple paper chart. If the reading starts creeping in one direction, the rule is already decided: swap the tool, adjust the offset, or tighten the clamp before the next run. That pre-made decision matters more than the chart itself, because it removes the temptation to wait for a confirmed failure.
Shift changes are another place where process stability quietly falls apart. A five-minute handoff routine—walking the machine, feeling for unusual heat or vibration, noting which adjustments were made, and marking the coolant level—keeps the incoming operator from starting blind. These small routines stick because they are concrete and immediate. They do not ask anyone to memorize a binder of procedures; they put the next correct action within arm's reach at the exact moment drift is trying to take hold.
Turning Steady Output Into a Lower Cost Per Part
Cost per part rarely drops because one shift manages to push the machine harder for an hour. It drops when the process settles into a rhythm that operators can trust, where material flows without last-minute expediting and the same number of finished pieces comes off the line day after day. That consistency spreads machine payments, labor, and overhead across more sellable parts, cutting the unit cost without a single change to the quoted cycle time.
Stable output also exposes which costs are actually tied to variability. Extra setups, safety stock, rework, and the time spent chasing missing parts all fade when throughput becomes predictable. By holding a steady pace, a shop can schedule tool changes around measured wear instead of reacting to scrap, run shorter queues, and stop paying for the chaos that uneven output tends to hide.
FAQ
It comes down to controlled rotation and heat distribution. If the mould moves at a steady, balanced speed through both axes and the oven temperature doesn't wander, the powder melts and lays down evenly. Independent arm speed settings help a lot when you're running asymmetric parts.
More than most people expect. A few degrees of overshoot can change how the material flows and fuses, so you end up with brittle spots or uneven inner surfaces. Good closed-loop control that responds quickly to oven load changes keeps the process stable without constant manual correction.
Yes, but it depends on the machine's rigidity and how well the mould is mounted. A solid frame reduces flexing during rotation, and adjustable mould arms let you fine-tune balance. That combination makes it easier to repeat dimensions on big tanks or bins without chasing settings between runs.
Controlled cooling is the bigger factor. If the part cools unevenly, it pulls itself out of shape. Machines that let you stage the cooling, with adjustable fans or water mist rather than a sudden quench, give the material time to shrink more uniformly. That reduces warpage and the soft spots that cause sink marks.
Don't copy the same recipe. Different grades have different melt flow and shrink behaviour, so peak oven temperature, cycle time, and cooling rate all need a small adjustment. Start with the material supplier's processing window, then make one change at a time and record the result until the inside surface looks smooth and the wall thickness evens out.
Keep an eye on the burner tips, air filters, and any seals around the oven. A partially blocked burner creates cold zones that don't show up until parts come out with thin areas. Checking rotation speeds and lubricating the arm pivots also prevents jerky movement that can disturb the melt.
Because the part is still forming while it cools. If you cool too fast, the outer skin solidifies before the inside, and the part can warp or develop internal stress. A slower, more uniform cooling step lets the material relax and shrink evenly, which means the next part behaves the same way.
Weigh a sample part and check wall thickness at the same spots every shift. A sudden weight drop usually means a change in powder charge or a blocked vent; thickness variation points to a heating or rotation problem. Keeping those numbers on a simple chart makes it easier to spot a trend before it becomes scrap.
Conclusion
Uniform wall thickness in rotomoulding is rarely a matter of finding the right machine setting and leaving it alone. Heating and cooling cycles can wander over a long run, so operators need to track temperature curves and cooling rates closely enough to catch drift before it turns into thin corners or warped openings. Mould design adds another layer: vent placement, parting line fit, and the way heat moves through the tool often matter more than oven set points. A machine that holds steady only becomes useful when those surrounding details are also kept in check.
Powder handling tends to get overlooked, yet dried, well-sized powder flows and fuses far more evenly than material that has picked up moisture or fines. Equally important are the small routines between cycles, such as confirming rotation speed, gas pressure, and cooling fan performance at regular intervals. These habits keep one shift from drifting away from the next. Once output settles into a repeatable rhythm, scrap rates fall and cycle times stop swinging, which brings the cost per part down without chasing faster cycles or compromising mould quality.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com