Tri-isobutyl Phosphate Supplier Evaluation Tips for Chemical Buyers
2026-11-03
Tri-isobutyl phosphate (TIBP) buyers often discover too late that 'lowest price' and 'reliable supply' rarely coexist. From hidden impurities to inconsistent batch quality, the wrong supplier can quietly erode your margins. The good news? A sharper evaluation process eliminates most of these risks before they reach your purchase order. Below, we break down the practical tips that procurement teams at Fortune use to vet TIBP suppliers—so you can stop guessing and start sourcing with certainty.
Look Beyond the Certificate of Analysis
A certificate of analysis gives you a snapshot, but it rarely tells the whole story. What happens to the material six months after it leaves the lab? How does it behave under real-world conditions, not just controlled test parameters? These are the questions that separate a reliable supplier from a merely compliant one.
Dig into how the product was actually made—not just what the final numbers say. Ask about raw material sourcing, process controls, and whether the same rigorous standards apply to every batch, not just the one that happened to be sampled. A single document can mask variability that shows up in your own production line.
Trust is built on consistency over time, not a single piece of paper. Look for evidence of ongoing monitoring, transparent failure investigations, and a willingness to share data beyond the minimum. If a supplier treats the certificate as the end of the conversation, that should tell you something.
Request a Split Sample from Their Latest Production Run
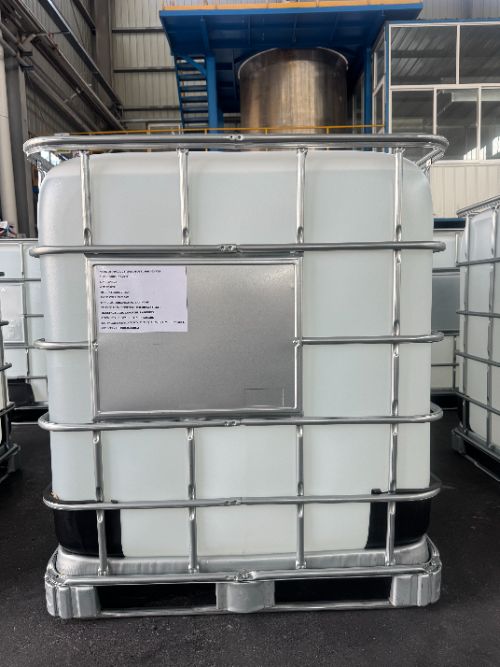
Before signing off on a bulk order, ask the supplier to pull a split sample from the most recent production run rather than a pre-production prototype. This catches raw material substitutions, rushed stitching, or coating inconsistencies that only appear once lines are running at full speed. It also gives you a realistic baseline for what will actually be boxed and shipped.
Be specific about where the split should be taken: front, middle, and end of the run if possible. Ask them to label each piece with the time and line number, then send photos of the unboxed sample against your approved spec. If the factory hesitates or sends a hand-picked golden piece, treat that as a red flag and push for a random draw instead.
Once the sample arrives, check it against the same criteria your QC team uses on the line—tolerances, weight, finish, packaging. Don't just eyeball it. Log discrepancies and request a corrective action note before the next run starts. This one extra step often costs nothing but can prevent a full shipment from being rejected at the port.
Trace Their Feedstock Sourcing for Tri-isobutyl Phosphate
对于磷酸三异丁酯,原料追溯往往从异丁醇的供应商开始。异丁醇的来源差异很大——有些来自石脑油裂解副产物的羰基合成,有些则来自玉米或甘蔗发酵。这两种路线在微量杂质和碳足迹上并不相同,而下游TiBP的酸值、色度和热稳定性会直接受到残留醛或水分的影响。因此,有经验的采购团队不会只核对一张分析证书,而是会要求供应商提供每一批次异丁醇的生产日期、储罐编号和运输记录,并定期抽取样本做气相色谱比对。
磷源同样值得细查。三氯氧磷或五氧化二磷的质量取决于磷矿的产地和净化工艺,某些矿源可能夹带砷、铁或硫酸盐。如果磷酸酯产品用于电子或医药中间体,这些杂质即使只有ppm级也可能引发客户投诉。部分TiBP制造商开始对磷源供应商进行现场审计,重点查看其矿石来源是否稳定、酸解和蒸馏步骤是否具备去除重金属的能力,并要求每季度更新一次第三方检测报告。
追溯工作最终要落到可操作的数据上。一些工厂建立了内部原料追溯表,把异丁醇和磷源的批号、到货日期、储罐位置以及对应TiBP成品批号串联起来。当某一批产品出现色度偏高或酸值波动时,工程师可以在几小时内回查是哪个原料批次出了问题,而不是花几天时间翻找纸质记录。这种做法虽然增加了仓储和文书成本,但对维持长期客户信任很有帮助,尤其在供应紧张、不得不更换原料供应商的时候。
Probe Their Control Limits for Acid Value and Water Content
Ask any supplier about their internal thresholds for acid value and moisture, and you'll quickly separate those who merely test from those who actually control. Many will cite standard limits from a data sheet, but the real question is how they arrived at those numbers and what happens when a batch drifts near the edge. Do they have alarm bands tighter than the specification? Do they re-test at multiple points during production, or only at the final drum? The answers reveal whether their limits are living, operational boundaries—or just paperwork.
Water content rarely behaves the same way across different resin batches or oil types, so a static single-point limit often hides hidden instability. A supplier with genuine process control will track moisture trends over time, flag upward drift before it hits the ceiling, and adjust drying or handling steps without waiting for an out-of-spec result. Acid value is trickier still: oxidation, hydrolysis, or contamination can push it up gradually, and a control limit that only triggers at the maximum allowable value is already too late for many downstream applications.
When you probe their limits, listen for specifics. Which analytical method do they use—Karl Fischer titration or loss-on-drying? What's their repeatability on acid value, and have they mapped variation across seasons, storage conditions, or incoming raw material lots? The strongest suppliers will show you not just the limit line, but the control chart behind it: center lines, warning bands, and documented actions taken before any batch ever reaches the edge.
Compare Handling and Shipping Records for Phosphate Esters
Different phosphate esters rarely ship under the same rules, and comparing handling or shipping records calls for more than a quick glance at the product name. Triphenyl phosphate, for instance, often moves as a non-hazardous solid under typical ambient conditions, while tributyl phosphate may fall under Class 9 due to environmental toxicity or require specific packing instructions when carried by air. Pull the safety data sheet and the transport document side by side, then check the UN number, packing group, and any special provisions. A record that lists only “phosphate ester” without the CAS number or specific isomer can hide exactly the differences that matter for safe handling.
Beyond classification, look at the physical state and the exposure controls noted in the handling records. High-viscosity aryl phosphates tend to be less volatile, so the records may emphasize spill containment and glove selection rather than vapor control. Lower-molecular-weight alkyl phosphates, by contrast, often show up with flash points below 93°C, which changes the packaging and segregation requirements. Shipping papers will reflect this through different proper shipping names, hazard labels, and sometimes marine pollutant marks. When comparing records, note whether the same ester appears under a generic entry or a more specific one, because that alone can alter the allowable container types and quantity limits.
A practical way to spot inconsistencies is to build a small matrix from the records: UN number, class, packing group, flash point, viscosity, and the stated PPE for handling. If two shipments of what is claimed to be the same phosphate ester show different entries, stop and verify the formulation—some commercial products are blends with additives that shift the hazard profile. Also check the revision dates on the documents. Older shipping records may predate updates to the IMDG Code or IATA Dangerous Goods Regulations, leading to a mismatch with current handling guidance. Keeping the comparison focused on the actual technical data, rather than the marketing name, prevents costly rejections and unsafe unloading practices.
Insist on a Pilot Test in Your Own Process Conditions
Every material behaves differently once it leaves the lab bench and enters your actual production line. Suppliers often share impressive pilot results obtained under tightly controlled conditions that rarely match your own operating reality—different humidity, raw material variability, equipment wear, or even shift-to-shift operator habits can shift outcomes significantly. Insisting on a pilot test in your own process conditions isn't about distrusting the vendor; it's about acknowledging that your plant has a unique fingerprint of temperature profiles, residence times, and mechanical stresses that no external trial can fully replicate.
A well-designed in-house pilot run reveals interactions you'd never see on a spec sheet. For instance, a filtration aid that worked flawlessly in a lab-scale beaker might blind your filter press because your slurry has a wider particle size distribution or a higher percentage of colloidal fines. Likewise, a catalyst that performs beautifully in a clean feedstock may foul rapidly when your process stream carries trace metals or dissolved polymers. By running the test under your own conditions, you capture these failure modes early, before they become expensive surprises at full scale.
The cost of skipping this step often shows up later as unplanned downtime, off-spec product, or emergency rework—expenses that dwarf the price of a focused pilot trial. Even a two-day test on a slipstream or a small side reactor can generate enough data to adjust operating parameters, redesign feed points, or select a more robust alternative. Ultimately, the only pilot data that matters is the data generated in the environment where the process will actually run, by the people who will run it day after day.
FAQ
Start with the supplier's technical capability and production consistency. TiBP is used in applications like metal extraction and flame retardants, so the supplier needs to demonstrate tight control over impurities and batch-to-batch uniformity. Ask for detailed specs and actual production records, not just a certificate.
Request a pre-shipment sample and have it analyzed by an independent lab. Compare results against the supplier's claim, focusing on acidity, moisture, and residual alcohol levels. Also ask about their internal QC frequency; a supplier that tests every batch is more reliable than one that tests only occasionally.
Yes. Depending on the destination country, you may need a Safety Data Sheet that follows GHS, a REACH registration if importing into the EU, and possibly a TSCA statement for the US. Don't accept vague assurances; ask for actual document numbers or copies.
Watch out for inconsistent pricing that's far below market average, unwillingness to share production details, or a lack of references from similar industries. Also, if the supplier changes its story about the manufacturing site or avoids a plant audit, treat it as a warning sign.
Very important, especially if you're moving bulk quantities. TiBP is sensitive to moisture and can degrade if stored improperly. Ask about packaging materials, nitrogen blanketing, and whether they use dedicated or lined containers. A supplier that treats it as just another solvent may not be protecting quality.
No. Low price often comes from cheaper raw materials or skipped purification steps, which can mean higher acid values or color issues. Instead, compare total cost including freight, import duties, potential rejections, and technical support. A slightly higher unit price can save money if it reduces downstream processing problems.
An on-site audit, whether virtual or in person, lets you confirm that they actually have the equipment and processes they claim. Look at storage tanks, reactor systems, and quality lab. If they're hesitant or give excuses, you're better off with a supplier who opens their doors.
Request a list of existing customers in similar applications and contact them. Ask about delivery consistency, how the supplier handled any quality complaints, and whether they communicated proactively. Also check how many years they've been producing phosphate esters specifically; longevity in this niche often indicates stability.
Conclusion
Chemical buyers often treat a certificate of analysis as the final word on tri-isobutyl phosphate quality, but that document only captures a narrow production moment. Ask the supplier for a split sample pulled from their most recent run and send it to an independent lab. You'll get a clearer picture of lot-to-lot consistency and whether their in-house numbers hold up. At the same time, ask where they source the raw alcohol and phosphorus oxychloride. A supplier that switches feedstocks without telling you can introduce trace impurities that alter downstream performance. Don't stop there—request their internal control limits for acid value and water content, and compare those to your own tolerance window. Tight limits on these two parameters usually indicate better hydrolysis stability and less corrosion risk in your process.
Logistics and real-world behavior matter just as much as spec sheets. Phosphate esters are hygroscopic and sensitive to handling, so review a supplier's shipping and storage records for temperature excursions, drum lining types, and inert gas blanketing. If you see repeated moisture spikes or damaged packaging in their history, that's a red flag. Finally, insist on a pilot test under your own process conditions—temperature, catalyst, residence time—before committing to a commercial order. A sample that performs well in their standard test may fail when it meets your specific system. Combining these checks gives you a supplier evaluation that goes far beyond a paperwork audit.
Contact Us
Contact Person: WANG SIHAI
Email: [email protected]
Tel/WhatsApp: +86-13815295628
Website: https://www.fortunechemtech.com/index_en.html